 English
Michael runs a factory in the southeast of Melbourne that specializes in producing dry-mixed mortar and special construction materials. Over the past two years, he has experienced a typical "growth pain": the order volume has increased, but the old production line not only occupied a large area but also frequently received warnings from the local environmental protection department due to dust from raw material transportation and inefficiency.
After multiple rounds of global supplier screening, Michael finally chose our "horizontal twin-shaft mixer + storage bin + open bag packaging machine" integrated solution. This solution not only addressed his environmental concerns but also increased his production capacity efficiency by 30%.
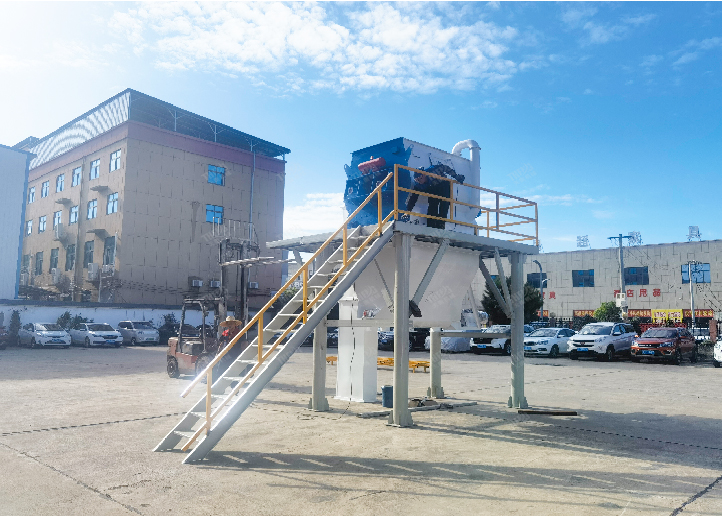
Limited space: The depth of the factory building is limited. If following the traditional layout, all equipment is placed on the ground and materials need to be transported horizontally multiple times, resulting in a large area occupation.
Environmental pressure: Australia has strict requirements for air quality in workplaces. The old equipment has poor sealing performance, and workers need to wear masks when operating, which also poses occupational health risks.
Low packaging efficiency: Previously, manual bagging and simple gate packaging were used, which was slow, had large weight errors, and resulted in a high rate of customer complaints.
1. Vertical and three-dimensional layout, saving space. Above the operation platform is the mixing machine, and below is the storage bin. The raw materials are lifted by the elevator and enter the top-mounted horizontal double-axis mixer. After the mixture is completed, the materials are directly discharged into the storage bin by gravity. The horizontal spiral conveyor is eliminated, saving approximately 35%-40% of the floor space.
2. Powerful shear force, easily handling high-viscosity formulations. The horizontal twin-screw mixer features opposed differential-speed rotating blades, which can create a strong material convection, easily handling viscous additives, eliminating dead corners, and achieving highly uniform mixing.
3. Smooth connection. The discharge door of the mixer directly connects to the feed inlet of the storage bin below. The storage bin serves as a buffer and storage function. The bottom of the bin is connected with the open pocket packaging machine, using double helix feeding + high precision sensor. The long distance transportation is omitted, the production efficiency is higher, the weighing is more accurate, and the stability of the product is guaranteed.
This production line only requires one forklift operator to load materials, and one operator to monitor the control panel and seal the packages to make it operational.
Precise material feeding. Through the electronic control system, raw materials are automatically lifted and fed into the horizontal double-axis mixer according to the formula.
High-speed mixing. The mixer operates for about 5-8 minutes (adjusted according to the formula) to complete uniform mixing. Gravity discharge and buffering. The pneumatic valve at the bottom of the mixer opens, and the finished product directly falls into the storage bin below the platform.
Automatic packaging. The bottom of the storage bin is connected to the packaging machine. Workers only need to place the open bags over the discharge port, trigger the foot switch, and the weighing system automatically completes rapid filling and slow replenishment. The bagging device ensures that no powder is lost during filling.
If you are also facing issues such as limited space, strict environmental inspections, or the desire to reduce losses during the transportation process, you might want to consider Michael's approach - making every step "vertical" and exploring the third dimension of profit potential.